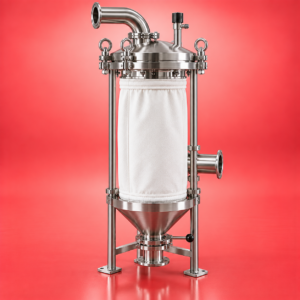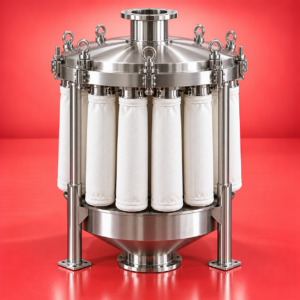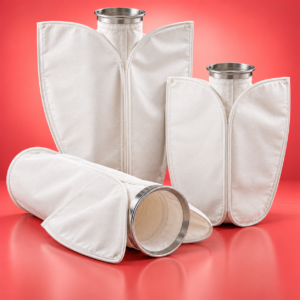
JMT Rubber manufactures Centrifuge Bags as specialized process components for pharmaceutical and industrial centrifuge applications. Designed for efficient solid-liquid separation, these bags are engineered to fit specific centrifuge equipment and process requirements.
Centrifuge Bags are particularly important in applications where reliable filtration, product recovery, contamination control, and compatibility with the processed material are essential.
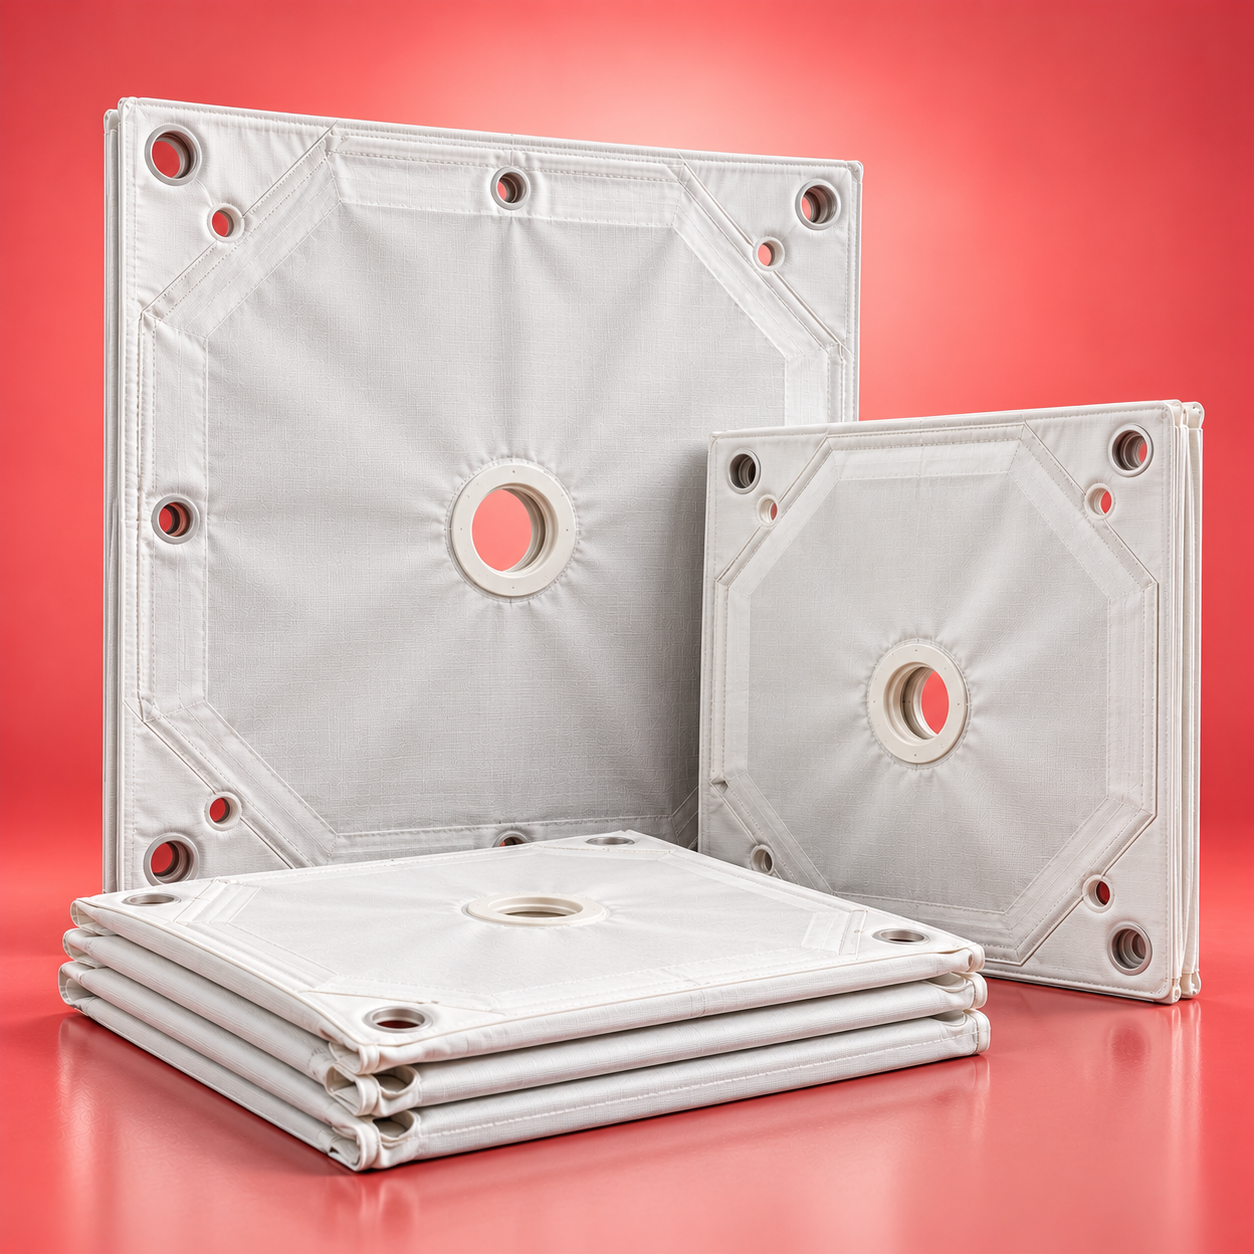
A Centrifuge Bag is a flexible filter bag installed inside a centrifuge basket. During centrifugation, the bag acts as a filtration medium, allowing the liquid phase to pass through while retaining the required solid material.
The bag is selected according to the centrifuge design, basket dimensions, filtration requirement, process material, operating conditions, and cleaning procedure.
Designed to support effective separation during centrifugation.
Manufactured according to the dimensions and configuration of the centrifuge basket.
Filter construction can be selected according to the required particle retention and process conditions.
Allows the bag to conform to the centrifuge basket during operation.
Suitable for controlled manufacturing environments where product integrity and process hygiene are important.
Available in application-specific dimensions, materials, and configurations.
The available JMT Rubber product information does not provide a detailed standard specification for Centrifuge Bags, including filter-media type, micron rating, standard dimensions, operating temperature, or pressure specifications.
These parameters should therefore be finalized according to the actual centrifuge and process.
Property | Specification |
Product | Centrifuge Bag |
Application | Centrifuge / Solid-Liquid Separation |
Filter Media | Application Dependent |
Material | Application Dependent |
Bag Dimensions | Centrifuge Specific |
Micron Rating | As Required |
Construction | Flexible Filter Bag |
Attachment | Equipment Specific |
Custom Manufacturing | Available |
JMT Rubber can develop Centrifuge Bags according to the customer’s equipment and filtration requirements.
For accurate product selection or manufacturing, provide:
An existing Centrifuge Bag or equipment drawing is recommended for replacement requirements.
Designed to support efficient retention and recovery of solid material.
Appropriate filter media can be selected according to the process requirement.
Custom dimensions help ensure proper fit within the centrifuge basket.
Replacement bags manufactured to equipment specifications can simplify maintenance.
Different materials and filter configurations can be considered for different applications.
JMT Rubber’s Centrifuge Bags provide equipment-specific filtration solutions for solid-liquid separation and product recovery across pharmaceutical, chemical, nutraceutical, food, and industrial processes.
A Centrifuge Bag is used as a filter medium inside a centrifuge basket to support solid-liquid separation and product recovery.
Yes. Bag dimensions, filter media, micron rating, and configuration can be selected according to the centrifuge and process requirements.
The centrifuge model, basket dimensions, process material, required particle retention, operating temperature, and cleaning conditions should be considered.
Yes. An existing bag, sample, drawing, or centrifuge specifications can be used to determine the appropriate replacement.
Provide the centrifuge make/model, basket dimensions, existing bag sample or drawing, filter-media requirement, micron rating, process material, and quantity.
Reliable fluid transfer solutions for critical manufacturing environments.
High-purity tubing for sensitive biological processes.
Precision tubing solutions for healthcare and medical equipment.
Safe and hygienic transfer systems for food-grade applications.
Flexible tubing solutions for dairy processing environments.
Contamination-free transfer of cosmetic ingredients and formulations.
Trusted tubing solutions for analytical and research applications.
Products manufactured in a controlled environment to ensure consistent quality and cleanliness.
Extensive experience serving pharmaceutical, biotech, medical, and food industries.
Tailored solutions developed to meet specific customer requirements.
Stringent quality control throughout the manufacturing process.
Expert guidance for product selection and application requirements.
Timely delivery and dependable customer support.
Contact our technical team to discuss your application requirements and discover for your equipment and process systems.